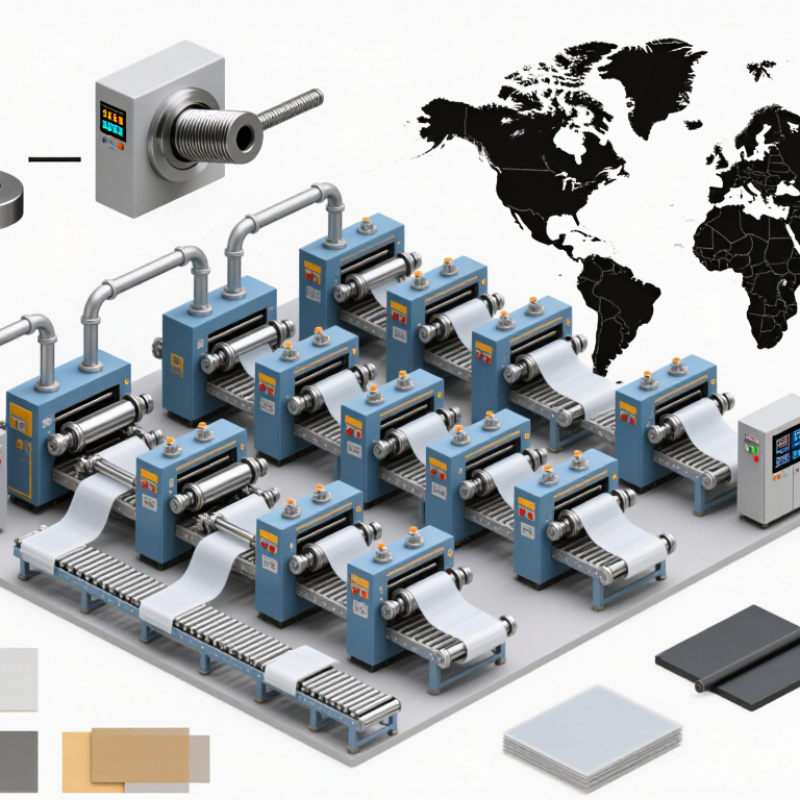
| Sheet Production Width | Standard flat-die extrusion line | 600–2,500 mm | Determines the maximum usable sheet width and production flexibility. | Confirm effective die width, edge-trim allowance, and maximum finished-sheet width in the technical offer. |
| Sheet Thickness Capability | Rigid PP sheet for packaging, printing, and industrial use | 0.5–12 mm | A wider thickness range allows one line to serve more applications. | Request trial samples at the thinnest, thickest, and most frequently produced thicknesses. |
| Material Compatibility | Polypropylene homopolymer, copolymer, and selected recycled PP blends | Virgin and approved recycled feedstock | Material flexibility can reduce raw-material costs and support sustainability targets. | Check the extruder screw design, melt-temperature range, and recommended material specifications. |
| Extrusion System | Single-screw extruder with flat T-die | Typically 90–180 mm screw diameter | The screw diameter and design influence output, melt uniformity, and energy consumption. | Review screw L/D ratio, motor rating, heating zones, and documented output at the target thickness. |
| Production Output | Output varies with width, thickness, formulation, and line speed | Approximately 100–800 kg/h | Output must match the buyer’s required annual capacity rather than only the maximum advertised value. | Compare guaranteed output using the buyer’s actual PP grade, sheet width, and thickness. |
| Thickness Control | Manual, semi-automatic, or automatic die-gap adjustment | Closed-loop control preferred for precision production | Stable thickness improves material yield, flatness, printing quality, and downstream performance. | Ask for thickness-tolerance data measured across the sheet width and along the production direction. |
| Cooling and Calibration | Three-roll calender, cooling table, or combined calibration system | Temperature-controlled rolls with adjustable line speed | Proper cooling affects surface finish, flatness, shrinkage, and dimensional stability. | Inspect roll diameter, temperature-control method, surface finish, and cooling-water requirements. |
| Line Speed | Speed depends on thickness, material, and required surface quality | Approximately 1–35 m/min | Higher speed can improve capacity, but only when sheet quality remains consistent. | Evaluate actual stable operating speed during a production trial instead of relying on no-load speed. |
| Sheet Surface Quality | Smooth, matte, embossed, or application-specific finish | Controlled by die, roll surface, temperature, and haul-off settings | Surface quality is important for packaging, thermoforming, printing, and lamination. | Define acceptable gloss, haze, scratches, roller marks, and surface contamination limits. |
| Automation Level | PLC control with touch-screen monitoring | Basic control to integrated automatic production management | Automation improves repeatability, operator safety, process monitoring, and production records. | Verify alarm functions, recipe storage, remote diagnostics, data logging, and user-access control. |
| Cutting and Stacking | Online trimming, fixed-length cutting, and automatic stacking options | Configured according to sheet size and packaging method | Integrated handling reduces manual labor and protects finished-sheet edges. | Confirm maximum stack height, cutting accuracy, transfer method, and finished-product packaging. |
| Energy Management | Variable-frequency drives, insulated heating zones, and efficient motors | Measured by kWh per kilogram of finished sheet | Energy consumption has a direct effect on operating cost and environmental performance. | Request a power-consumption estimate based on the intended PP formulation and production rate. |
| Quality and Safety Compliance | Electrical, mechanical, and guarding requirements for the target market | Applicable local regulations and internationally recognized standards | Compliance supports safer operation, import clearance, and customer audits. | Review electrical drawings, safety-guarding details, emergency-stop tests, and conformity documents. |
| Factory Acceptance Testing | Trial production before shipment | Recommended for every customized line | Testing verifies output, thickness stability, surface quality, and machine integration before delivery. | Use a signed acceptance protocol covering raw material, operating conditions, test duration, and results. |
| Installation and Commissioning | Remote guidance or on-site technical service | Usually scheduled after utilities and auxiliary equipment are ready | Professional commissioning reduces start-up delays and prevents incorrect operating settings. | Confirm service scope, technician availability, travel requirements, training hours, and commissioning checklist. |
| Spare Parts and After-Sales Support | Recommended spare-parts list, troubleshooting, and technical documentation | Support period and response time defined contractually | Accessible support helps maintain uptime and simplifies long-term maintenance. | Request a parts list for the first two years, response-time commitments, manuals, and wiring diagrams. |
| Customization Capability | Options for width, thickness, embossing, co-extrusion, and downstream handling | Configured to the product specification | Customization avoids paying for unsuitable capacity and supports future product expansion. | Compare the proposed configuration with a written product specification and layout drawing. |


 Close