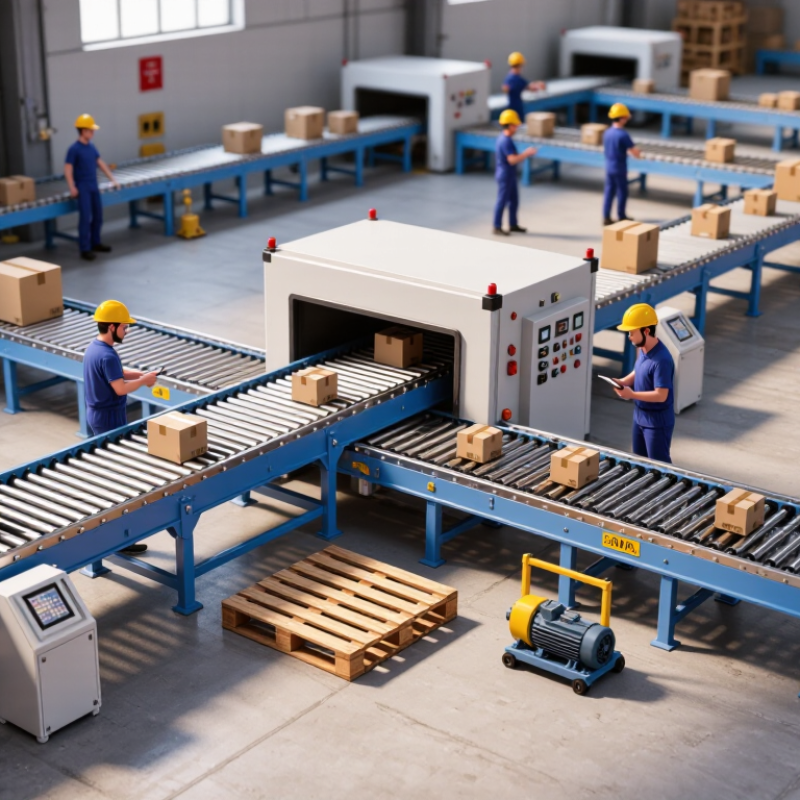
| 1 | Define the load first | Gravity, powered, or chain-driven roller conveyor | The conveyor must carry the heaviest individual unit and the total accumulation load without excessive deflection. | Select a rated capacity above the maximum operating load, not only the average load. Include pallet, carton, container, or tote weight. | Common light- to medium-duty systems handle approximately 50–250 kg per unit; heavier systems require reinforced frames and rollers. | Confirm unit weight, load distribution, base condition, impact during loading, and the required safety factor with the supplier. |
| 2 | Match the roller diameter to the load | Gravity or powered roller conveyor | Rollers must provide adequate contact area and resist bending under the working load. | Small cartons may use smaller rollers, while pallets and heavy containers normally require larger-diameter rollers and stronger shafts. | Typical roller diameters include about 38, 50, 60, 76, and 89 mm, depending on load and frame design. | Check roller material, wall thickness, shaft diameter, bearing type, roller load rating, and deflection under full load. |
| 3 | Choose the correct roller pitch | Gravity, powered, and accumulation roller conveyor | The product should rest on enough rollers at all times to remain stable and move smoothly. | A common design rule is to maintain at least three rollers under the shortest rigid load during transport. | Typical center-to-center pitches range from approximately 50–150 mm; heavier or irregular loads usually need closer spacing. | Provide the shortest package length, package base dimensions, product rigidity, and required transfer orientation. |
| 4 | Select gravity or powered operation | Gravity roller versus motor-driven roller conveyor | Gravity systems need manual pushing or a controlled slope; powered systems provide consistent movement and automation. | Use gravity for simple, low-throughput movement. Use powered rollers for long lines, high throughput, controlled speed, or accumulation. | Powered conveying commonly operates around 0.1–0.5 m/s, but the required speed depends on product stability and process timing. | Confirm throughput per hour, conveyor length, elevation change, start-stop frequency, noise limits, and available power supply. |
| 5 | Check conveyor width and product fit | All roller conveyor types | The conveyed unit must remain supported and guided without rubbing the frame or falling between side rails. | For straight conveying, the usable roller width is commonly selected slightly wider than the product base width. | Typical conveyor widths range from approximately 300–1,200 mm, with custom widths available for oversized loads. | Measure maximum and minimum product width, base shape, side-clearance needs, guide-rail position, and transfer points. |
| 6 | Consider curves and transfers | Tapered-roller curve or multidirectional transfer section | Curves require stable product tracking, while transfers must bridge gaps without catching package edges. | Use tapered rollers for curved paths and ball-transfer or pop-up units when products must change direction or conveyor line. | Curve radius, roller taper, transfer gap, and product center of gravity affect tracking and safe operation. | Submit a layout drawing, product dimensions, turning direction, minimum turning radius, and transfer-height tolerances. |
| 7 | Specify the operating environment | Painted steel, galvanized steel, or stainless-steel conveyor | Moisture, dust, chemicals, temperature, and washdown conditions determine the suitable materials and protection level. | Use corrosion-resistant construction in humid or wet areas and sealed components where dust or liquid ingress is expected. | Stainless steel is commonly preferred for frequent washdown or hygienic environments; surface treatment depends on exposure. | State ambient temperature, humidity, washdown method, chemical exposure, dust level, indoor/outdoor location, and cleanliness requirements. |
| 8 | Plan accumulation and product control | Zero-pressure accumulation or zoned powered roller conveyor | Products may need to queue without collision, back pressure, package damage, or uncontrolled release. | Use individually controlled zones with sensors for fragile goods, automated lines, and variable production flow. | Zone length is often based on the longest load plus clearance; sensor logic and release spacing must match throughput. | Confirm product fragility, accumulation quantity, release sequence, sensor type, control interface, and emergency-stop arrangement. |
| 9 | Verify motor, drive, and electrical standards | Belt-driven, chain-driven, or motorized roller conveyor | The drive system must provide sufficient starting torque and match the destination country's electrical requirements. | Variable-speed drives are useful where line speed changes, while fixed-speed drives suit simple material-flow applications. | Common industrial supplies include 230 V or 400 V three-phase power at 50 or 60 Hz, depending on the market. | Confirm voltage, frequency, phase, motor protection, control voltage, plug and wiring requirements, documentation, and local compliance. |
| 10 | Evaluate safety, maintenance, and total cost | Any conveyor type, configured for the site's risk level | The system should be safe to operate, easy to inspect, and economical throughout its service life. | Include guarding, emergency stops, pinch-point protection, access clearance, spare parts, installation, and training in the purchase decision. | Maintenance access should allow inspection of bearings, rollers, chains, belts, sensors, and drive components without unsafe exposure. | Request manuals, risk assessment information, spare-parts lists, warranty terms, service response details, and installation requirements. |


 Close