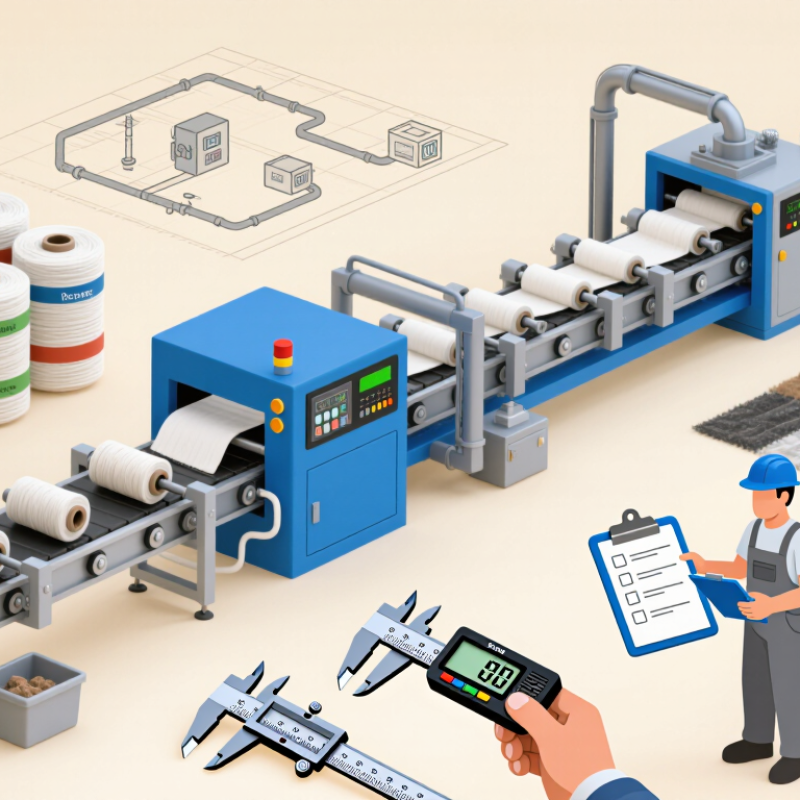
| Compact pilot or small-scale line | 1.6–2.5 m | 30–80 m/min | Approximately 0.5–2.0 tonnes/day, depending on basis weight and line configuration | Viscose, polyester, cotton, wood pulp blends, and other short staple fibers | Typically 25–60 mm for carded web formation | Sampling, product development, specialty wipes, and limited-volume production | Best for testing |
| Standard carded-web spunlace line | 2.5–3.6 m | 80–150 m/min | Approximately 2–6 tonnes/day, depending on basis weight, hydroentanglement energy, and drying efficiency | Viscose, polyester, cotton, lyocell, polypropylene, and blends | Typically 25–60 mm; fiber crimp and fineness must match the carding system | Wet wipes, dry wipes, medical fabrics, hygiene products, and general industrial nonwovens | General-purpose choice |
| High-capacity carded-web line | 3.6–5.0 m | 120–220 m/min | Approximately 5–12 tonnes/day, subject to basis weight, working width, and number of carding machines | Viscose, polyester, cotton, lyocell, polypropylene, and recycled fiber blends | Typically 25–60 mm; consistent staple length is important for high-speed web uniformity | Large-volume wipes, filtration media, medical disposables, automotive fabrics, and hygiene substrates | Best for volume |
| Crosslapper-based heavy-weight line | 2.5–5.0 m | 30–100 m/min | Approximately 2–10 tonnes/day, depending on web weight and layering ratio | Polyester, polypropylene, viscose, cotton, recycled fibers, and durable blends | Typically 40–80 mm; longer fibers can improve web integrity when properly carded | Geotextiles, upholstery, filtration, construction materials, and absorbent structures | Best for heavy fabrics |
| Airlaid and spunlace combination line | 2.0–4.0 m | 30–120 m/min | Approximately 1–8 tonnes/day, depending on pulp content, basis weight, and bonding sequence | Wood pulp, fluff pulp, viscose, lyocell, cotton, polyester, and bicomponent fibers | Airlaid pulp is generally much shorter than staple fibers; staple components are commonly 25–60 mm | Absorbent wipes, cleaning materials, medical pads, and high-absorbency nonwovens | For absorbency |
| Recycled-fiber spunlace line | 2.5–4.0 m | 60–150 m/min | Approximately 2–7 tonnes/day, depending on fiber cleanliness, opening quality, and blend ratio | Recycled cotton, recycled polyester, recycled viscose, and virgin-fiber blends | Often 20–60 mm after recycling; fiber length distribution should be checked before purchase | Wipes, cleaning cloths, shoe materials, automotive interiors, and industrial fabrics | Requires trials |
| Biodegradable-fiber spunlace line | 2.5–4.0 m | 60–150 m/min | Approximately 2–7 tonnes/day, depending on fiber blend and drying requirements | Viscose, lyocell, cotton, PLA, cellulose-based fibers, and biodegradable blends | Typically 25–60 mm for staple fibers; moisture sensitivity and thermal limits must be evaluated | Flushable or dispersible wipes, personal-care products, biodegradable wipes, and packaging materials | Check fiber behavior |
| Continuous-filament spunlace line | 2.5–4.5 m | 80–200 m/min | Approximately 3–10 tonnes/day, depending on filament denier, basis weight, and line width | Continuous polyester, polypropylene, viscose, lyocell, and other suitable filament materials | Not applicable in the staple-fiber sense; filament denier, orientation, and tow opening are critical | High-strength wipes, filtration, medical fabrics, synthetic leather substrates, and technical textiles | For filament products |


 Close