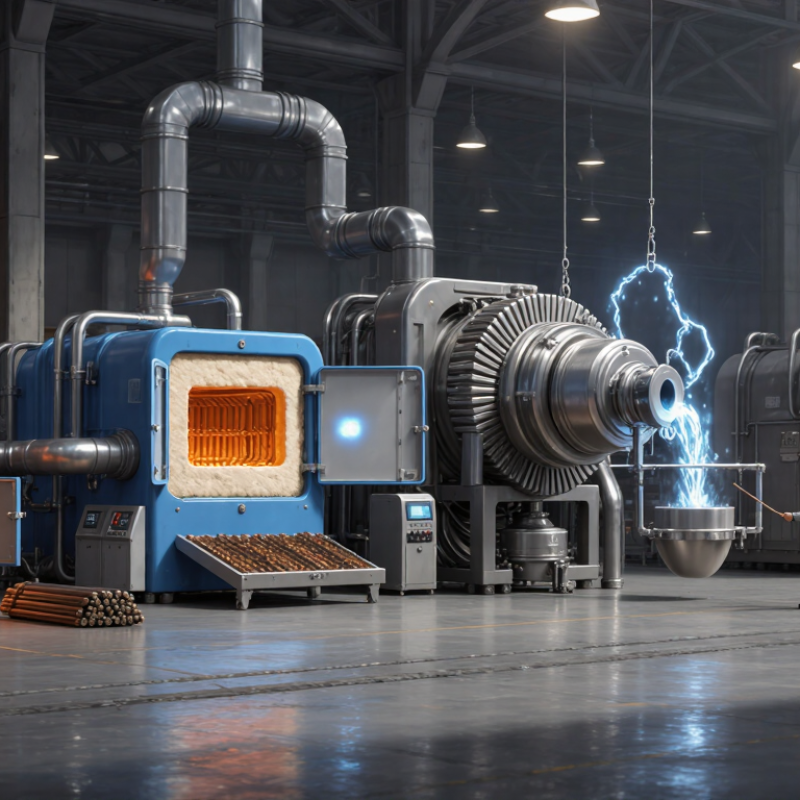
| Gas-Fired Reverberatory Furnace | High-volume primary or secondary aluminium melting; common in foundries and remelting operations. | Approximately 1–100 tonnes per batch, depending on furnace design. | Uses natural gas, LPG, or other gaseous fuels. Energy use is strongly affected by charge density, door openings, furnace insulation, and exhaust heat recovery. | High throughput and large bath surface; suitable for continuous or batch operation. Longer heat-up and melt cycles than induction systems are typical. | Flame supervision, automatic fuel shut-off, combustion-air interlocks, pressure monitoring, refractory inspection, molten-metal containment, and controlled charging. | Produces combustion emissions, including carbon dioxide and nitrogen oxides. Regenerative or recuperative burners and exhaust filtration can reduce fuel use and emissions. | Large plants where high capacity, fuel availability, and heat recovery justify the installation. |
| Electric Resistance Furnace | Batch melting, holding, heat treatment, and applications requiring a clean, quiet furnace environment. | Approximately 50 kg to 10 tonnes, with larger custom installations available. | Converts electrical energy into heat through resistance elements. On-site combustion emissions are very low, but total carbon impact depends on the electricity source. | Good temperature uniformity and precise control; melting speed is usually moderate and depends on installed power and insulation quality. | Electrical isolation, over-temperature protection, door and lid interlocks, element protection, grounding, and safe handling of molten metal. | No direct fuel-combustion emissions at the furnace. Fume extraction is still required for fluxes, coatings, contaminated scrap, and metal treatment operations. | Small and medium foundries, recycled aluminium operations, and facilities with low-carbon or renewable electricity. |
| Coreless Induction Furnace | Rapid melting of clean or prepared aluminium charge for foundry production and flexible alloy changes. | Approximately 100 kg to 10 tonnes per furnace, with larger systems possible for specialized operations. | Electromagnetic induction heats the metal directly. Electrical efficiency is generally high, but performance depends on power factor, coil condition, refractory thickness, and furnace loading. | Fast melting, strong bath circulation, and good process control. Excessive electromagnetic stirring can increase oxidation or dross if the process is not controlled. | Water-cooling flow and temperature monitoring, ground-leakage protection, coil insulation checks, emergency power-off, refractory monitoring, and spill containment. | No direct combustion emissions. Local extraction remains necessary for dross, fluxes, oil-contaminated scrap, and metal-treatment fumes. | Flexible production with frequent alloy changes, high melting rates, and a reliable electrical supply. |
| Channel Induction Furnace | High-volume melting and holding where a stable molten-metal supply is required. | Commonly used from several tonnes to more than 50 tonnes, depending on the plant configuration. | Designed for efficient holding and continuous operation. Electrical demand is relatively steady when the furnace is kept full and well insulated. | Excellent for continuous melting and holding; the channel unit normally works with a separate charging or melting section. | Cooling-system monitoring, leak detection, refractory integrity checks, electrical protection, controlled tapping, and emergency metal-transfer procedures. | No direct combustion emissions. Energy and emissions performance depend primarily on electricity generation and the efficiency of continuous operation. | High-throughput plants requiring stable temperature, continuous delivery, and low holding losses. |
| Rotary Melting Furnace | Recycling of aluminium scrap with coatings, oxides, mixed shapes, or relatively high contamination levels. | Approximately 1–30 tonnes per batch, depending on the refractory lining and rotation system. | Usually fuel-fired, although hybrid and electrically assisted systems are available. Rotating action improves heat and material contact but can increase dross if poorly managed. | Good adaptability to difficult scrap and high metal recovery potential when charge preparation, flux practice, and rotation speed are optimized. | Guarding of moving parts, burner interlocks, controlled rotation, safe door operation, refractory inspection, spill protection, and operator exclusion zones. | Requires effective dust and fume capture because painted, oily, or coated scrap can generate significant particulate and gaseous emissions. | Recycling lines handling variable or contaminated scrap where metal recovery is more important than the shortest melt cycle. |
| Tilting Crucible Furnace | Small-batch melting and precise pouring for casting shops, laboratories, and flexible production cells. | Approximately 20 kg to 2 tonnes per batch. | Available with gas, electric resistance, or induction heating. Specific energy use is usually higher at small scale because of surface-area and holding losses. | Offers controlled transfer and good flexibility for short production runs; capacity and melting rate are limited compared with industrial reverberatory systems. | Two-hand or guarded tilting controls, mechanical stops, secure crucible support, over-temperature protection, and dedicated molten-metal splash barriers. | Electric versions have no direct combustion emissions; all versions require ventilation for fluxes, coatings, dross, and potential metal-treatment fumes. | Flexible, low-to-medium-volume production where compact size and controlled pouring are priorities. |
| Dual-Chamber or Sealed-Chamber Melting Furnace | Recycling operations seeking improved separation between charging, melting, and clean-metal holding zones. | Generally used for medium to high production rates; capacity is configured to match the scrap stream and casting demand. | Can use gas, electricity, or a hybrid arrangement. Reduced exposure of clean molten metal can lower oxidation and metal losses. | Improves process separation, metal quality, and recovery when charging conditions vary. | Pressure and atmosphere control, automatic doors, gas monitoring where applicable, interlocked transfer systems, emergency drainage, and robust fume extraction. | Enclosed charging and controlled exhaust can reduce fugitive emissions, oxidation, and dross generation; filtration remains necessary for contaminated scrap. | Modern recycling plants prioritizing metal recovery, reduced oxidation, process automation, and emissions control. |


 Close