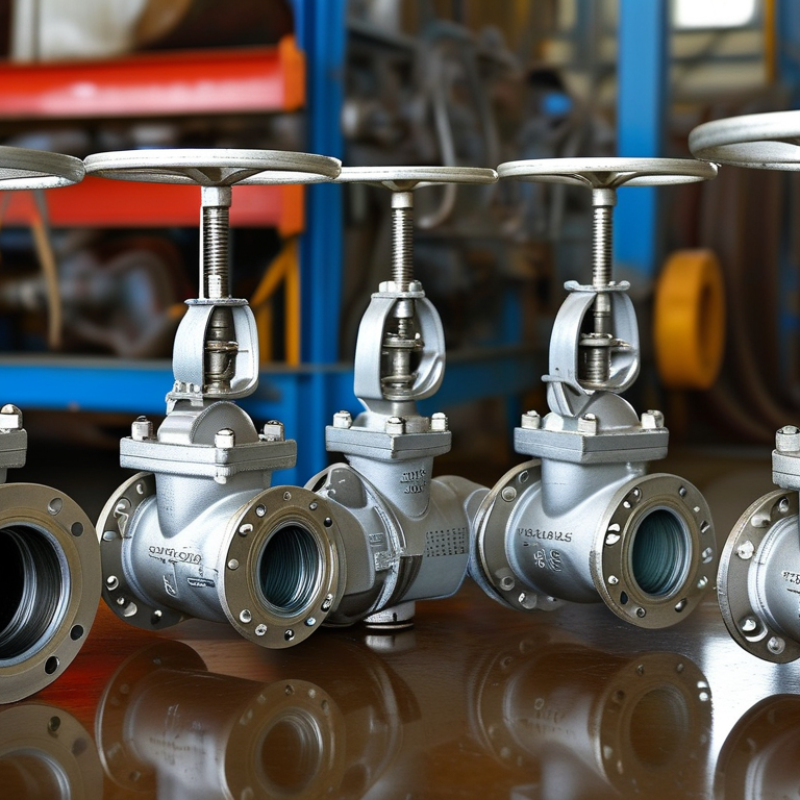
| Application and Valve Type | Confirm whether the design is wafer, swing, lift, dual-plate, piston, or axial flow. | The selected type should match flow direction, installation position, pressure pulsation, backflow risk, and available space. | Technical datasheet, flow schematic, installation drawing, and application references without confidential customer information. | 8% |
| Applicable Design Standard | Check the design standard stated in the quotation and drawing. | The standard must be suitable for the service. Common references include API 594 for check valves, API 6D for pipeline valves, and ASME B16.34 for pressure-containing valve requirements. | Design calculation, standard compliance statement, certified drawings, and clause-by-clause deviation list. | 10% |
| Pressure Class and Size | Verify nominal size, pressure class or PN rating, end connection, and face-to-face dimensions. | All dimensions must match the approved piping specification. Pressure-temperature ratings must be based on the actual body and trim materials. | General arrangement drawing, pressure-temperature chart, flange standard, and dimensional inspection report. | 8% |
| Body and Bonnet Material | Review material grade, corrosion resistance, temperature range, and service compatibility. | Typical material choices include carbon steel such as ASTM A216 WCB for general service, low-temperature carbon steel such as ASTM A352 LCB for cold service, and stainless steel such as ASTM A351 CF8M for corrosive applications. Final selection must follow the process medium and design temperature. | Material test certificate, heat number traceability, chemical composition, mechanical properties, and impact-test records where required. | 12% |
| Disc, Plate, Seat, and Trim | Check trim material, surface treatment, hardness, wear resistance, and compatibility with the medium. | Trim materials should be clearly identified by grade. Hard-facing or corrosion-resistant overlays should include thickness, hardness, and inspection requirements where specified. | Part-level material certificates, hardness reports, coating or overlay reports, and spare-parts list. | 8% |
| Pressure Testing | Confirm shell, seat, and low-pressure closure tests. | Testing should follow the contractually agreed standard, such as API 598 or ISO 5208. The test medium, pressure, holding time, leakage class, and acceptance result must be recorded. | Factory test certificate, calibrated gauge records, test procedure, and inspection release note. | 14% |
| Leakage Performance | Determine the required seat leakage level for the process and shutdown function. | The purchase order should state the required leakage class or allowable leakage rate. “Zero leakage” should not be accepted as an undefined marketing term; it must be linked to a test standard and test pressure. | Seat-test results, test curves where applicable, and an agreed leakage acceptance table. | 10% |
| Flow and Pressure-Loss Data | Evaluate cracking pressure, pressure drop, flow coefficient, and reverse-flow behavior. | The supplier should provide test-based or validated engineering data. A low cracking pressure is desirable where pump protection and energy efficiency are important, but it must not compromise stable closure. | Flow test data, pressure-drop curve, cracking-pressure value, and calculation assumptions. | 8% |
| Manufacturing Process Control | Review casting, forging, machining, welding, heat treatment, and assembly controls. | Critical processes should be documented, traceable, and subject to inspection hold points. Weld repairs, if permitted, should require an approved repair procedure and inspection record. | Quality plan, process flow chart, welding procedure qualifications, heat-treatment charts, and nonconformance records. | 10% |
| Non-Destructive Examination | Confirm the required inspection method for castings, forgings, welds, and pressure boundaries. | Typical methods include visual inspection, liquid penetrant, magnetic-particle, radiographic, and ultrasonic examination. The method and sampling level should be specified before production. | NDE procedures, examiner qualifications, reports, acceptance criteria, and weld or casting traceability. | 8% |
| Quality Management System | Assess document control, corrective actions, inspection independence, and production consistency. | A current ISO 9001 certificate from an accredited certification body is a positive indicator, but it should be verified and supported by an on-site or remote quality audit. | Certificate scope, latest audit summary, quality manual index, inspection organization chart, and corrective-action records. | 8% |
| Traceability and Documentation | Check whether each pressure-retaining and critical component can be traced to its material heat and inspection result. | Heat numbers, part identification, drawings, test reports, and packing records should remain consistent throughout the manufacturing and delivery documents. | Manufacturing record book index, nameplate photo, material certificates, inspection reports, and final dossier sample. | 6% |
| Inspection and Acceptance Plan | Define buyer, third-party, and supplier inspection points before manufacturing starts. | The inspection plan should identify hold points for material review, dimensional inspection, NDE, pressure testing, coating, marking, and final release. | Inspection and test plan, approved quality plan, witness-point schedule, and final inspection checklist. | 5% |
| Packaging and Corrosion Protection | Review end protection, internal cleanliness, desiccant use, lifting points, and export packaging. | Valve openings should be protected, machined surfaces preserved, identification retained, and packaging suitable for the planned transport and storage period. | Packing specification, photographs before shipment, preservation procedure, and packing list. | 3% |
| Commercial and Lifecycle Value | Compare total cost rather than purchase price alone. | Consider delivery time, inspection cost, spare parts, maintenance access, warranty terms, replacement lead time, and documented failure history. | Detailed quotation, warranty conditions, spare-parts quotation, lead-time schedule, and lifecycle-cost comparison. | 3% |


 Close