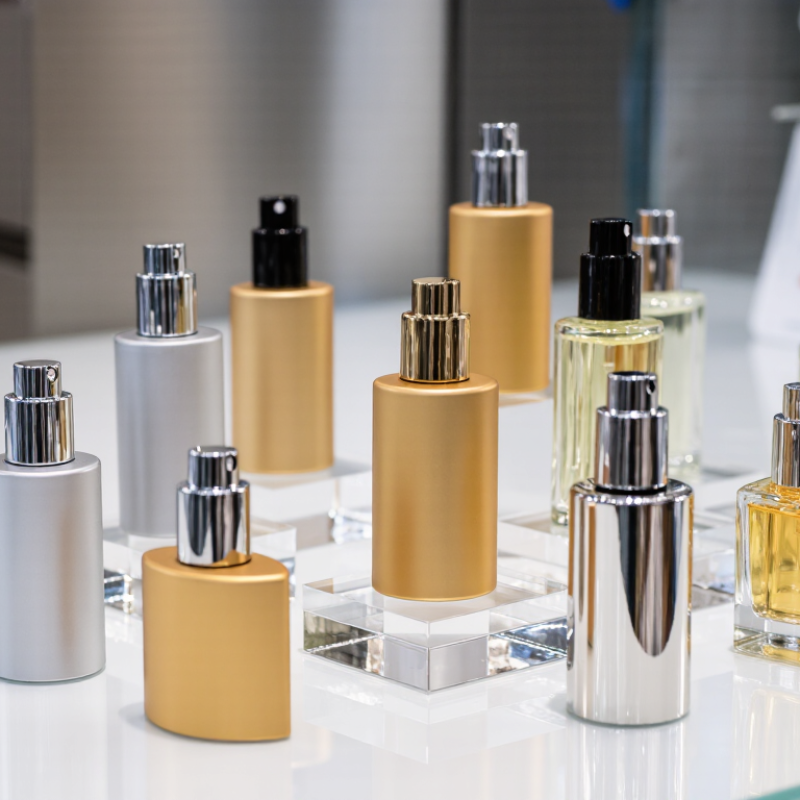
| Bottle Material | Common aluminum grades include 1050, 3003, and 5052, selected according to forming, strength, and surface requirements. | Aluminum sheet or slug is cut, stamped, impact-extruded, or deep-drawn into the required bottle body. | Aluminum is lightweight, opaque, recyclable, and provides protection from light exposure that can affect fragrance appearance and stability. | Request the exact alloy designation, temper, material certificate, and recycled-content statement where applicable. |
| Typical Capacity Range | Approximately 10–200 mL for travel, sample, personal-use, and premium fragrance formats. | The designer defines the internal volume, external dimensions, shoulder profile, base geometry, and center of gravity before tooling. | Capacity influences product positioning, shipping cost, portability, and compatibility with pumps and closures. | Confirm nominal fill volume, brimful capacity, tolerance, and the required fill line with the packaging supplier. |
| Wall and Base Design | Wall thickness is design-dependent; many formed aluminum packages use thin, lightweight walls with a reinforced base and neck area. | Finite-element analysis, forming trials, and dimensional inspection are used to balance rigidity, weight, and manufacturability. | The structure must resist denting, deformation, leakage, and damage during filling, transport, and consumer handling. | Ask for wall-thickness maps, compression results, drop-test conditions, and allowable cosmetic dents. |
| Internal Protection | A compatible internal coating or lacquer may be used when the fragrance formula requires additional chemical resistance. | The formed body is cleaned, treated, coated, and cured under controlled time and temperature conditions. | The internal barrier helps reduce direct contact between the fragrance formula and the aluminum surface. | Require formula-compatibility testing, coating specification, cure records, and extractables or migration evaluation when relevant. |
| Neck and Closure Compatibility | Crimp, screw, or custom neck systems may be used; the finish must match the selected pump, valve, collar, and cap. | The neck is formed or machined to controlled diameter, height, roundness, and sealing dimensions. | A precise neck finish supports reliable crimping, spray performance, leak prevention, and consistent assembly. | Verify neck drawings, pump compatibility, crimp dimensions, torque requirements, and assembled leak-test results. |
| Surface Finishing | Available finishes commonly include anodizing, spray coating, metallic coating, satin brushing, polishing, and protective clear coating. | Surface preparation is followed by coloring or coating, curing, and visual inspection under defined lighting conditions. | The finish creates the visual identity while improving scratch resistance and perceived product quality. | Approve a master color standard and check gloss, adhesion, abrasion resistance, color deviation, and coating uniformity. |
| Decoration Options | Screen printing, pad printing, hot stamping, offset printing, laser marking, embossing, and debossing are widely used. | Decoration is applied after forming and surface treatment, with registration controls for curved or tapered bodies. | Aluminum supports both minimalist unprinted designs and high-contrast premium graphics. | Evaluate artwork accuracy, ink or foil adhesion, barcode readability, abrasion resistance, and batch-to-batch color consistency. |
| Leak and Pressure Testing | Testing methods may include vacuum, pressure, inverted-storage, thermal-cycle, and assembled-package leakage tests. | Samples are tested after filling or with a validated test medium; results are compared with approved acceptance criteria. | Fragrance leakage can damage labels, cartons, dispensing components, and surrounding products. | Request written test methods, sample quantities, acceptance limits, and reports from production-equivalent samples. |
| Dimensional Quality Control | Critical checks include height, diameter, neck finish, wall thickness, roundness, weight, volume, and decoration position. | Calipers, gauges, coordinate-measuring equipment, weighing systems, and visual standards are used during inspection. | Tight dimensional control improves pump fit, assembly efficiency, shelf appearance, and filling-line performance. | Confirm inspection frequency, sampling plan, calibrated equipment, control plans, and certificate-of-analysis availability. |
| Sustainability Profile | Aluminum is widely recyclable, and recycled content can reduce the material’s primary-production energy demand; actual benefits depend on sourcing and processing. | Manufacturers can reduce impact through lightweighting, scrap recovery, recycled feedstock, efficient coating systems, and optimized transport packaging. | Sustainability claims must reflect the complete package, including coatings, pumps, caps, labels, and material separation. | Ask for recycled-content evidence, environmental declarations where available, scrap-recycling data, and clear disposal guidance. |
| Compliance Documentation | Relevant documentation may include material declarations, restricted-substance statements, quality certificates, packaging specifications, and traceability records. | Compliance is managed through documented specifications, approved raw materials, batch records, inspections, and corrective-action procedures. | Document control supports market access, retailer requirements, product safety reviews, and consistent future production. | Check alignment with applicable requirements such as REACH, packaging regulations, ISO-based quality systems, and destination-market rules. |


 Close